Top Flow Regulator Valve Manufacturers and Suppliers in the Market

By:Admin on 2025-01-09 03:15:08

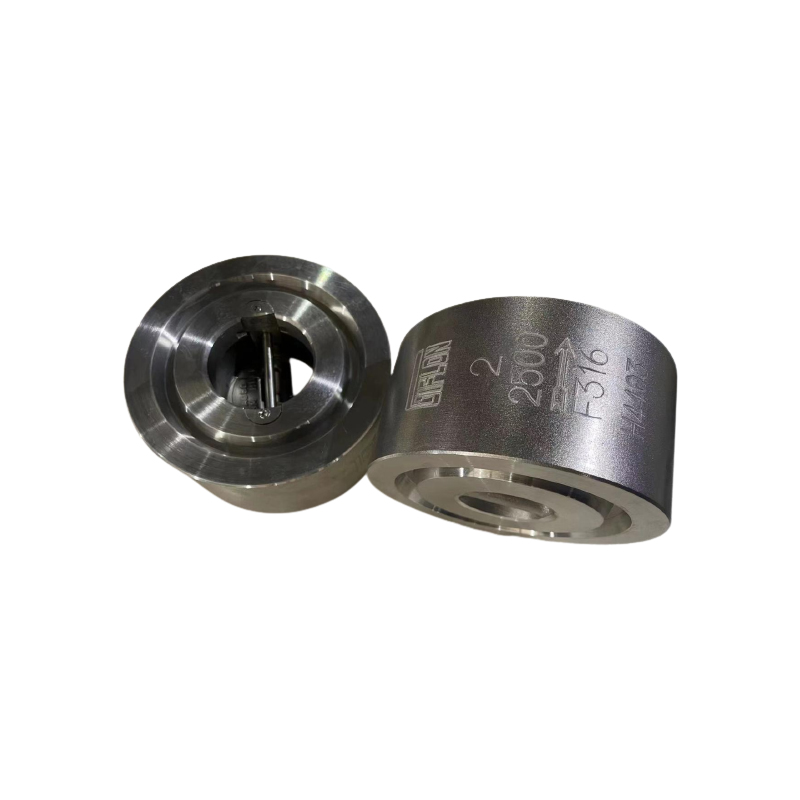
Flow Regulator Valve Factories in the United States have been thriving in recent years, thanks to the high demand for their products in various industries. These factories play a crucial role in manufacturing and supplying flow regulator valves that are essential for controlling and regulating the flow of gases and liquids in different applications.One of the leading flow regulator valve factories in the country is (Company Name), a renowned manufacturer with a strong reputation for producing high-quality and reliable flow control products. The company has been in the business for over 30 years and has established itself as a trusted supplier to a wide range of industries, including oil and gas, water treatment, chemical processing, and manufacturing.(Company Name) takes pride in its state-of-the-art manufacturing facilities and a team of dedicated engineers and technicians who are committed to delivering top-notch products that meet the highest standards of quality and performance. The company's relentless pursuit of excellence and innovation has enabled it to stay ahead of the competition and remain a preferred choice for customers seeking superior flow regulator valves.The success of (Company Name) and other flow regulator valve factories can be attributed to the increasing demand for flow control solutions across different sectors. In the oil and gas industry, for example, flow regulator valves are essential for maintaining operational efficiency and safety in various processes, such as oil refining, pipeline transportation, and natural gas distribution.Similarly, the water treatment industry relies on flow regulator valves to ensure the proper flow and distribution of water in treatment plants, as well as for wastewater management. In chemical processing plants, these valves are critical for controlling the flow of various chemicals and ensuring precise measurements for production purposes.Moreover, flow regulator valves are extensively used in manufacturing operations, where they help regulate the flow of fluids and gases in different production processes, such as food and beverage processing, pharmaceutical manufacturing, and automotive assembly lines. As a result, the demand for high-quality flow regulator valves continues to grow, driving the success of factories like (Company Name).One of the key factors contributing to the success of flow regulator valve factories is their ability to adapt to changing industry requirements and technological advancements. (Company Name), for instance, continuously invests in research and development to enhance its product offerings and introduce innovative solutions that cater to the evolving needs of its customers.In addition to developing advanced flow regulator valve technologies, (Company Name) focuses on sustainability and environmental responsibility in its manufacturing processes. The company is dedicated to ensuring that its products not only meet industry standards but also adhere to environmental regulations, thereby promoting a greener and more sustainable approach to flow control solutions.Furthermore, flow regulator valve factories like (Company Name) prioritize customer satisfaction by offering comprehensive support services, technical assistance, and customized solutions to meet specific application requirements. By maintaining strong relationships with its customers and providing exceptional after-sales support, the company has earned a reputation for reliability and trustworthiness in the industry.Looking ahead, the future looks promising for flow regulator valve factories as they continue to evolve and innovate to meet the growing demands of various industries. With a focus on quality, performance, and sustainability, companies like (Company Name) are well-positioned to play a vital role in ensuring efficient and reliable flow control solutions for years to come.In conclusion, the success of flow regulator valve factories in the United States, such as (Company Name), reflects the increasing importance of flow control solutions across industries. By prioritizing innovation, quality, and customer satisfaction, these factories have cemented their position as key suppliers of essential flow regulator valves, driving operational efficiency and safety in a wide range of applications. As the demand for reliable flow control solutions continues to grow, these factories are poised to play a crucial role in shaping the future of various industries.

Read More
Durable and Reliable Soft Sealed Gate Valves for Industrial Applications

By:Admin on 2025-01-06 04:46:48

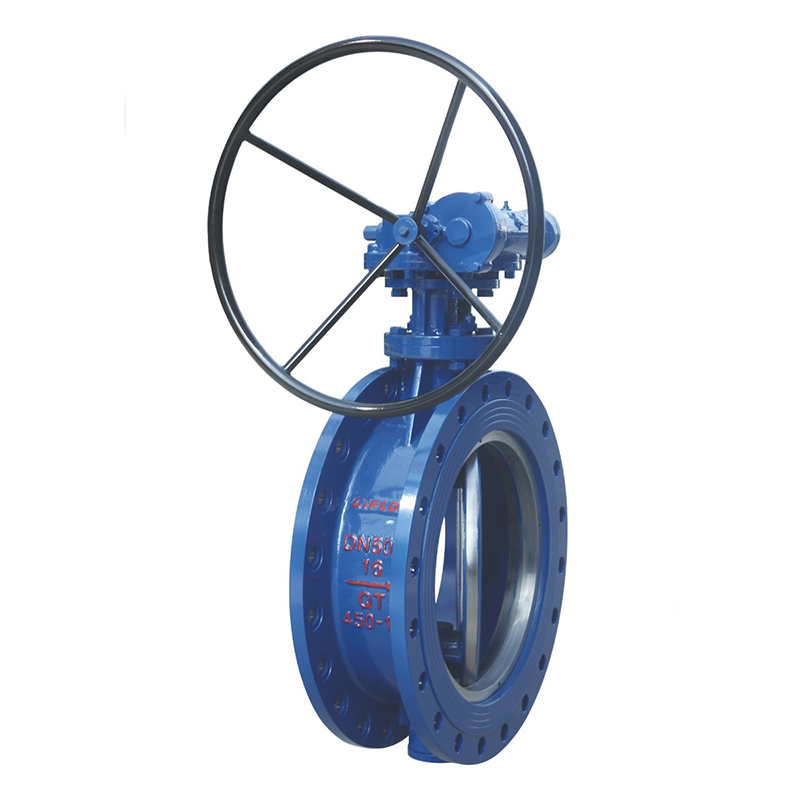
Soft Sealed Gate Valve: A Reliable Solution for Efficient Flow ControlIn industrial applications where efficient flow control is essential, having a reliable and durable valve system is crucial. One company has been at the forefront of providing top-quality valves for various industries, and their soft sealed gate valve has been making waves for its superior performance and innovative design.{Company Name}, a leading manufacturer of industrial valves, has been serving the needs of the global market for over two decades. With a commitment to quality, innovation, and customer satisfaction, the company has established itself as a trusted name in the industry.The soft sealed gate valve offered by {Company Name} is a testament to their dedication to providing high-quality solutions for flow control. This type of valve is specifically designed to handle the challenges of controlling the flow of various media in industrial settings. Its unique design features a gate with a soft sealing element, which provides a tight and reliable seal, ensuring efficient performance and minimal leakage.One of the key advantages of the soft sealed gate valve is its ability to effectively control the flow of different types of media, including water, oil, gas, and chemicals. This versatility makes it a preferred choice for a wide range of applications across industries such as oil and gas, water treatment, chemical processing, and power generation.The superior performance of the soft sealed gate valve can be attributed to its innovative design and high-quality construction. {Company Name} utilizes advanced manufacturing techniques and premium materials to ensure that each valve meets the highest standards of quality and reliability. With a focus on precision engineering and strict quality control, the company has earned a reputation for producing valves that deliver exceptional performance in even the most demanding environments.In addition to its unrivaled performance, the soft sealed gate valve offered by {Company Name} is also known for its durability and longevity. Built to withstand the rigors of industrial operations, these valves are designed to provide reliable service over an extended period, minimizing the need for frequent maintenance and replacement.Furthermore, {Company Name} prides itself on offering customized solutions to meet the specific requirements of its clients. Whether it's a standard size valve or a custom-designed solution, the company has the capability to deliver products that align with the unique needs of each customer.The commitment to customer satisfaction doesn't end with the sale of the valve. {Company Name} also provides excellent after-sales support, including technical assistance, maintenance services, and spare parts availability. This comprehensive approach ensures that customers can rely on the continued performance of their valves and maximize their operational efficiency.As industries continue to evolve and demand high-performance solutions for flow control, the soft sealed gate valve from {Company Name} remains a reliable choice for companies seeking quality, durability, and efficiency in their valve systems. With a solid track record of delivering cutting-edge solutions and a commitment to excellence, {Company Name} is well-positioned to meet the evolving needs of the global market for industrial valves.In conclusion, the soft sealed gate valve offered by {Company Name} represents a reliable and efficient solution for flow control in industrial applications. With its innovative design, superior performance, and commitment to quality, this valve is poised to continue making a significant impact in a wide range of industries, cementing {Company Name}'s position as a leader in the field of industrial valves.

Read More

Motorized Ball Valve: Everything You Need to Know

By:Admin on 2025-01-02 03:09:21

OEM Motorized Ball Valve a Game Changer in the IndustryIn the constantly evolving world of industrial automation, there is a growing demand for high-quality and reliable components that can improve efficiency and streamline processes. This is where OEM Motorized Ball Valve comes into play.With a strong focus on innovation and technological advancement, OEM Motorized Ball Valve has established itself as a leader in the industry. The company's dedication to quality and performance has made it a go-to choice for businesses looking to enhance their automation systems.Through the utilization of cutting-edge technologies and engineering expertise, OEM Motorized Ball Valve has developed a range of motorized ball valves that offer unmatched precision and reliability. These valves are designed to meet the most demanding industrial applications, ensuring smooth operation and consistent performance.The company's commitment to excellence extends beyond just its products. With a team of highly skilled professionals, OEM Motorized Ball Valve provides exceptional customer service and technical support. This level of dedication has earned the company a reputation for being a trusted partner in the industry, capable of delivering tailored solutions to meet the specific needs of its clients.One of the key factors that sets OEM Motorized Ball Valve apart from its competitors is its ability to provide custom solutions. The company understands that every industrial application is unique, and therefore offers bespoke valve designs to suit individual requirements. This level of flexibility has earned OEM Motorized Ball Valve a loyal customer base, as businesses appreciate the ability to create tailored solutions that perfectly fit their automation systems.In addition to its commitment to quality and customization, OEM Motorized Ball Valve places a strong emphasis on sustainability and environmental responsibility. The company's valves are designed to maximize energy efficiency and minimize waste, helping businesses to reduce their carbon footprint and operate in a more eco-friendly manner.Furthermore, OEM Motorized Ball Valve is continuously investing in research and development to stay ahead of the curve. By staying at the forefront of technological advancements, the company is able to offer the latest innovations to its customers, giving them a competitive edge in their respective industries.The success of OEM Motorized Ball Valve can be attributed to its unwavering dedication to excellence, innovation, and customer satisfaction. The company's relentless pursuit of perfection has established it as a trailblazer in the industrial automation sector, and its products are widely regarded as game-changers that have revolutionized the industry.With a strong foundation built on quality, reliability, and unmatched expertise, OEM Motorized Ball Valve is poised to continue leading the way in the world of industrial automation. As the demand for cutting-edge automation solutions continues to grow, the company is well-positioned to meet the evolving needs of its customers and drive innovation in the industry.In conclusion, OEM Motorized Ball Valve has set the bar high for excellence in the industrial automation sector. With its unwavering commitment to quality, customization, sustainability, and innovation, the company is a force to be reckoned with. As businesses continue to seek advanced automation solutions to improve their processes, OEM Motorized Ball Valve will undoubtedly remain a trusted partner that delivers exceptional value and performance.

Read More